Corrugated boxes are a primary choice for industrial and commercial packaging due to their durability, 비용 효율성, and recyclability. This article explores what industries are corrugated boxes used for, detailing applications across food, 전자상거래, 의약품, 전자 장치, and heavy industries. The analysis provides actionable insights for supply chain managers, packaging engineers, and procurement professionals seeking optimal packaging solutions.
골판지 상자는 어떤 산업에 사용됩니까?? A Broad Overview
| 산업 / Sector | Key Packaging Needs & Functions | Typical Corrugated Solutions |
| 음식 & 음료 | Hygiene, 수분 조절, retail-ready display, cold-chain compatibility | Wax-coated boxes, moisture‑resistant liners |
| E‑Commerce & 소매 | Custom branding, protective shipping, modular sizing, easy returns | Printed mailer boxes, multi-depth cartons |
| Pharmaceutical & 헬스케어 | Sterile protection, temperature control, tamper-evident features, traceability | Insulated corrugated, partitioned medical boxes |
| 전자 장치 & Consumer Goods | Shock/moisture protection, anti-static properties, global shipping compliance | Anti‑static lined boxes, cushioned inserts |
| Industrial & Automotive | Heavy-duty stacking strength, hazardous material compliance, pallet compatibility | Triple-wall corrugated, UN‑certified export boxes |
| Chemicals & Hazardous Materials | Containment of liquids/powders, regulatory labeling (예를 들어, GHS), weather resistance | Coated corrugated, reinforced bulk containers |
Food and Beverage Industry
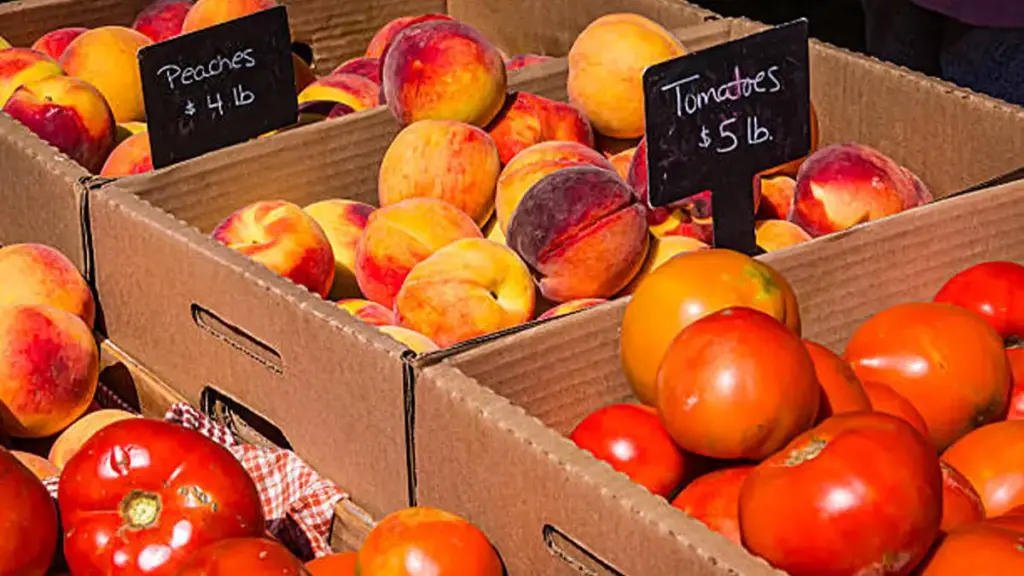
Corrugated packaging is widely adopted in the food and beverage industry because it balances cost-efficiency, hygiene, and regulatory compliance. Its lightweight yet durable structure supports high-speed packaging lines and meets strict safety standards, 포함 FDA and EU regulations on materials intended for food contact.
Practical applications include:
- Fresh Produce: Single-wall corrugated trays or ventilated cartons enhance airflow, maintaining freshness during cold-chain transport.
- Bottled Beverages: Double-wall boxes with moisture-resistant coatings prevent damage from condensation during storage and distribution.
- Packaged Snacks and Confectionery: Custom-printed corrugated boxes function as retail-ready displays, reducing restocking time and improving brand visibility.
Using corrugated packaging in these categories offers significant benefits: high recyclability rates (often exceeding 90%), reduced contamination risks compared to reusable crates, and compatibility with automated palletizing systems. For businesses assessing what industries are corrugated boxes used for, the food and beverage sector demonstrates how optimized packaging design directly supports product integrity and supply chain efficiency.
E‑Commerce and Retail
E‑commerce and retail sectors rely heavily on corrugated packaging due to its structural strength, 비용 효율성, and customizability. The rapid growth of online shopping and omnichannel distribution models demands packaging that can protect goods through multi-stage handling while maintaining branding consistency. Corrugated boxes meet global testing standards such as ISTA 3A for parcel delivery and are widely adopted by programs like Amazon Frustration-Free Packaging (FFP).
Practical applications include:
- Subscription Boxes: Lightweight single-wall corrugated mailers reduce shipping costs and support vibrant digital printing for branding.
- Electronics Fulfillment: Double-wall cartons with custom inserts ensure shock absorption during long-distance delivery.
- Retail-Ready Displays: Die-cut corrugated boxes enable rapid shelf placement in brick-and-mortar stores, improving merchandising efficiency.
Industry studies show corrugated solutions can lower packaging costs by 15–20% while reducing damage claims in transit. For companies evaluating what industries are corrugated boxes used for, the e‑commerce and retail sectors highlight how optimized box design enhances fulfillment speed, supports brand perception, and meets both sustainability and durability requirements in high-volume logistics networks.
Pharmaceutical and Healthcare
The pharmaceutical and healthcare industries adopt corrugated packaging primarily to ensure product integrity, sterility, and regulatory compliance during distribution. Packaging must meet stringent standards such as ISO 15378 for medicinal product packaging and Good Distribution Practices (GDP) to maintain quality throughout the supply chain.
Practical applications include:
- Vaccine Transport: Triple-wall corrugated boxes combined with thermal liners preserve temperature stability during cold-chain logistics.
- Medical Devices: Partitioned cartons protect fragile instruments and support tamper-evident sealing.
- Prescription Medicines: Moisture-resistant boxes safeguard blister packs and bottles against humidity during export.
Corrugated packaging offers recyclability exceeding 85% and reduces contamination risk compared to reusable crates. Its lightweight construction lowers freight costs while complying with pharmaceutical serialization and labeling requirements, making it indispensable for companies analyzing what industries are corrugated boxes used for within regulated medical markets.
전자 및 소비재
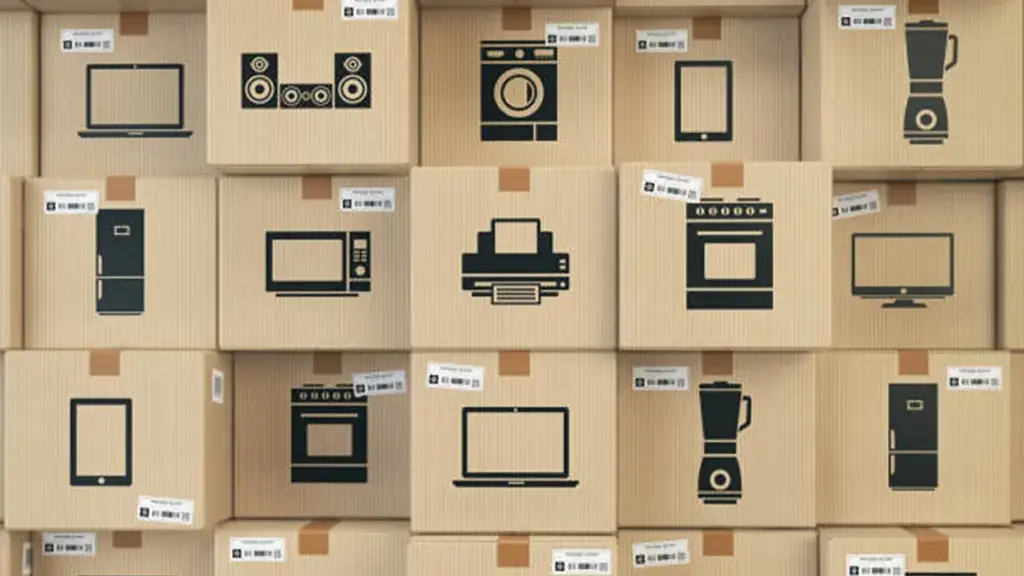
Corrugated packaging serves the 전자 장치 and consumer goods industries by providing shock resistance, 수분 조절, and efficient global shipping performance. Devices and components demand packaging that withstands vibration and static discharge, complying with ISTA 2A/3A transit testing and anti-static material guidelines.
Practical applications include:
- 가전제품: Anti-static lined boxes protect smartphones, tablets, and accessories during cross-border e-commerce fulfillment.
- Home Appliances: Heavy-duty double-wall cartons with foam inserts reduce transit damage for mid-sized appliances.
- Premium Retail Packaging: High-quality print finishes enhance brand presence for small consumer goods and personal care items.
Corrugated solutions lower damage rates by up to 25% compared to non-corrugated options and support sustainable branding goals through high recyclability. These benefits illustrate why electronics remain a significant focus when assessing what industries are corrugated boxes used for.
Industrial, Automotive, and Chemical Sectors
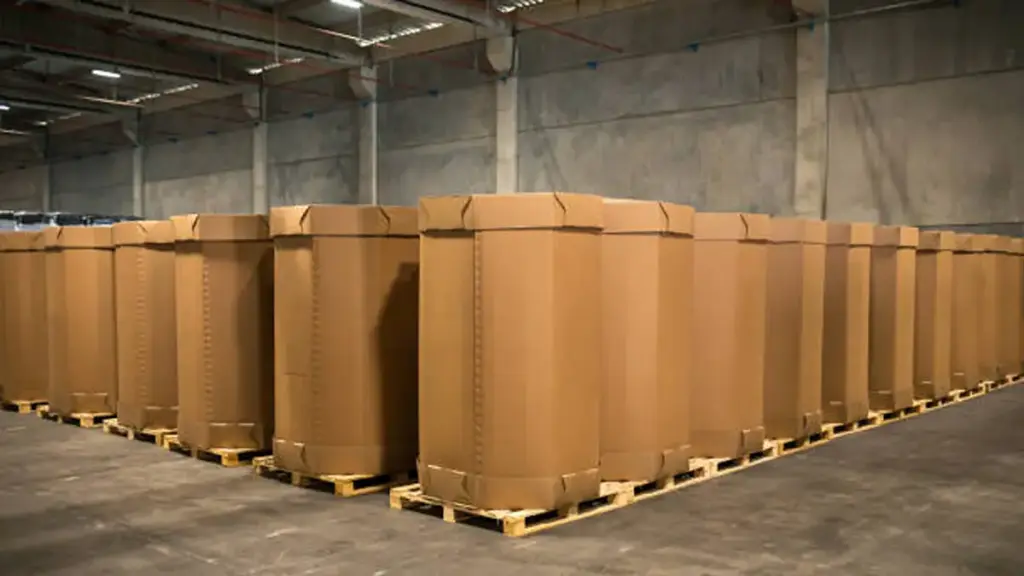
Corrugated boxes are critical for heavy industries requiring high stacking strength, hazardous material compliance, and export-ready durability. Triple-wall corrugated constructions can rival wooden crates while reducing weight and meeting UN/DOT packaging standards for hazardous goods transport.
Practical applications include:
- Automotive Components: Engine parts and transmissions shipped in reinforced corrugated bulk containers compatible with pallets.
- Chemical Products: Coated corrugated boxes handle lubricants or powders while adhering to GHS labeling requirements.
- Industrial Machinery: Customized inserts support secure transit of precision components in multi-modal logistics.
These solutions optimize supply chain efficiency by enabling safer handling and reducing freight costs. Their recyclability and adaptability across sectors underscore their relevance in what industries are corrugated boxes used for, particularly where durability and regulatory adherence are paramount.
Sustainability and Future Trends in Corrugated Packaging Across Industries
Sustainability is reshaping corrugated box uses across all sectors. Most boxes are 70–100% recycled fiber and fully recyclable after use, supporting circular economy goals. Innovations include lightweighting (reducing material without sacrificing strength), digital printing for small-batch customization, and integration of smart packaging features like QR codes for traceability.
Market forecasts predict continued growth, driven by e-commerce expansion and stricter environmental regulations. According to Smithers’ market report, global corrugated packaging demand will exceed $300 10억 단위로 2027. Understanding what industries are corrugated boxes used for helps businesses align procurement and design strategies with these evolving sustainability trends.
결론
Corrugated packaging continues to serve as a foundation across industries, combining durability, 비용 통제, 지속 가능성. From food and pharmaceuticals to electronics and automotive, its adaptability ensures compliance with varied operational and regulatory standards. For businesses assessing what industries are corrugated boxes used for, partnering with experienced suppliers is essential. packccp delivers optimized corrugated solutions tailored to sector-specific needs, enabling reduced waste and improved logistics efficiency.
Contact PackCCP today to explore custom designs that align with your supply chain and sustainability goals.