Moving a folding carton design from approved dieline to mass production exposes gaps that flat-screen reviews miss: crease scores that crack on the folder-gluer, glue flaps that miss the adhesive wheel, or board grain that fights every fold on high-speed filling equipment.
This guide walks through the technical decisions that determine whether your folding carton design converts cleanly at volume — structural geometry, board caliper selection, print method trade-offs, 仕上げの互換性, and the supplier criteria that separate a reliable packaging partner from a costly one.
What Makes a Good Folding Carton Design
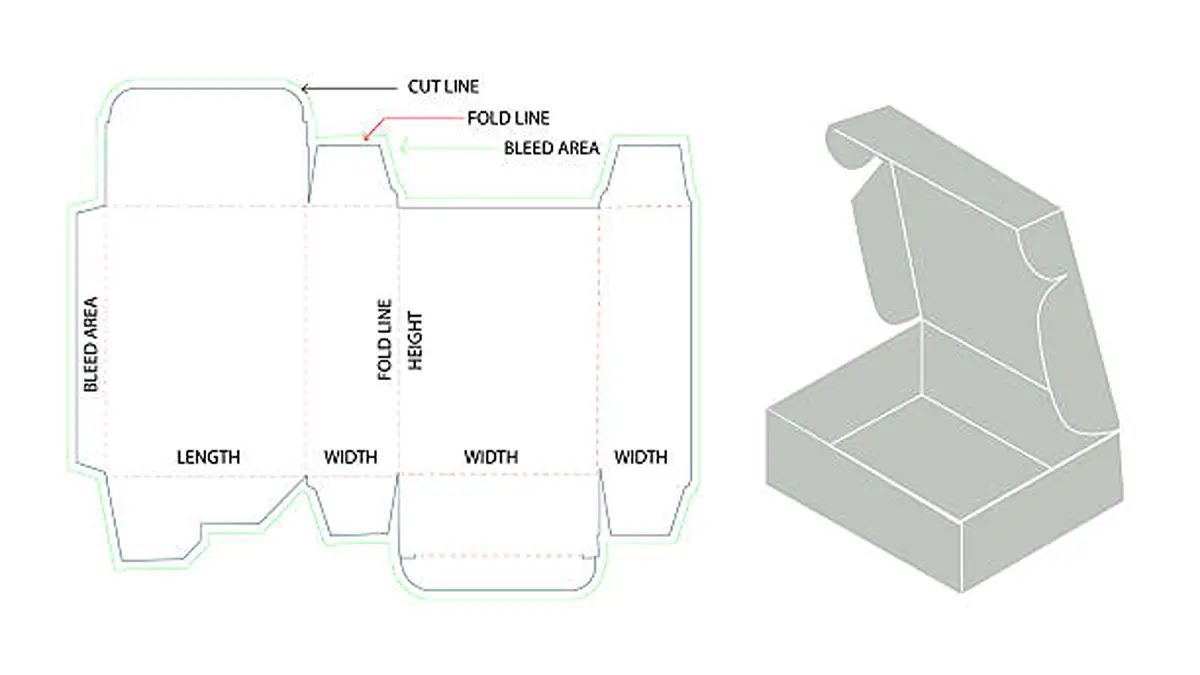
A well-engineered folding carton design balances four constraints: 製品の保護, line efficiency, shelf presence, and unit cost — resolved before production tooling is cut, not after.
Structural Performance and Manufacturing Integration
A carton must protect its contents and run reliably on automated equipment. These dual requirements demand that you match material specifications to the product weight, 脆弱性, and filling-line speed before committing to production.
- Material Alignment: Coordinate paperboard caliper, bending stiffness, and grain direction to support product weight and prevent panel bulging on the filling line.
- Style Selection: Choose auto-bottom, reverse-tuck, or snap-lock configurations based on whether your filling line runs manual or automated erection.
- Geometry Verification: Test flat dieline geometry, crease scores, and glue-tab margins with unprinted physical mockups before ordering production tooling.
- Sheet Utilization: Optimize blank nesting and pallet patterns to reduce converting trim waste and improve material yield.
If the blank cannot run on the folder-gluer without jamming, no amount of graphic refinement will prevent costly downtime.
Graphic Execution and Recyclability
Packaging serves as both a brand touchpoint and a recyclable material. Designers must lay out visual assets and specify finishing treatments that support fiber recovery at end of life.
- Information Hierarchy: Establish clear text contrast and respect safe-zone margins on the dieline to prevent copy from wrapping into crease lines.
- Recyclable Finishes: Select coatings and varnishes that protect against scuffing without interfering with standard repulping.
- Functional Access: Integrate pull-tabs, thumb notches, and reclosable tucks to improve the consumer opening experience.
- Circular Sourcing: Specify responsibly sourced fiber board and eliminate unnecessary plastic windows to simplify material sorting.
Dieline Design Essentials for Folding Cartons
Accurate dieline geometry — fold allowances, glue flap dimensions, and prepress tolerances — determines whether a carton converts cleanly or generates score cracks and glue failures on the production line.
| Dieline Element | Standard Tolerance | Operational Purpose |
|---|---|---|
| Glue Flap Width | 18 – 22 mm | Ensures stable adhesive coverage on high-speed folder-gluers. |
| Glue Flap Bevel | 7 – 10 degrees | Prevents flap interference and improves machine clearance. |
| SBS Substrate Thickness | 0.35 – 0.60 mm | Matches bending stiffness to structural transport loads. |
| Fold Allowance | 1 board thickness per 90° fold | Prevents warping and maintains accurate outer dimensions. |
| Artwork Bleed | Minimum 3 mm | Compensates for sheet movement during die cutting. |
| Safe-Zone Inset | 3 – 4 mm | Protects text and barcodes from folding friction. |
| Trapping Tolerance | 0.15 – 0.25 mm | Manages plate registration variation on multi-color offset runs. |
Structural Anatomy and Material Tolerances
A flat dieline converts to three dimensions only when board thickness offsets and flap clearances are calculated correctly. Four parameters demand tight coordination:
- Glue Flap Geometry: Design glue flaps at 18 – 22 mm with a 7 – 10 degree bevel. This angle prevents folder-gluer collision and ensures clean machinery clearance.
- Grain Direction: Align the grain parallel to major fold axes. Folding against the grain increases crack risk on coated boards, especially at calipers above 0.45 mm.
- Fold Allowance: Calculate using one board thickness per 90-degree fold. This maintains correct outer dimensions and prevents structural warping during erection.
- Crease Geometry: Coordinate crease rule height, matrix width, and board caliper to eliminate shallow scores that cause uneven folding resistance and joint failures.
For a detailed breakdown of how dielines translate from 2D file to 3D carton, read our companion guide on what is a dieline in packaging.
Prepress Integration and Quality Validation
Moving from digital artwork to production tooling requires strict prepress controls. Without physical validation, press-run drift will compromise the final folded assembly.
- Bleed and Safe Zones: Maintain a minimum 3 mm bleed beyond outer cut paths. Preserve a 3 – 4 mm safe-zone inset to keep text, barcodes, and regulatory copy away from high-friction folds.
- Dieline Layering: Isolate technical dielines on a dedicated locked artboard layer using non-printing spot colors set to overprint.
- Trapping Tolerances: Implement trapping between 0.15 そして 0.25 mm to manage sheet movement during multi-color offset runs without distorting fine details.
- Validation Testing: Subject physical prototypes to industry-standard compression and vibration testing per IoPP-recommended protocols to verify joint strength and closure performance before committing to production tooling.
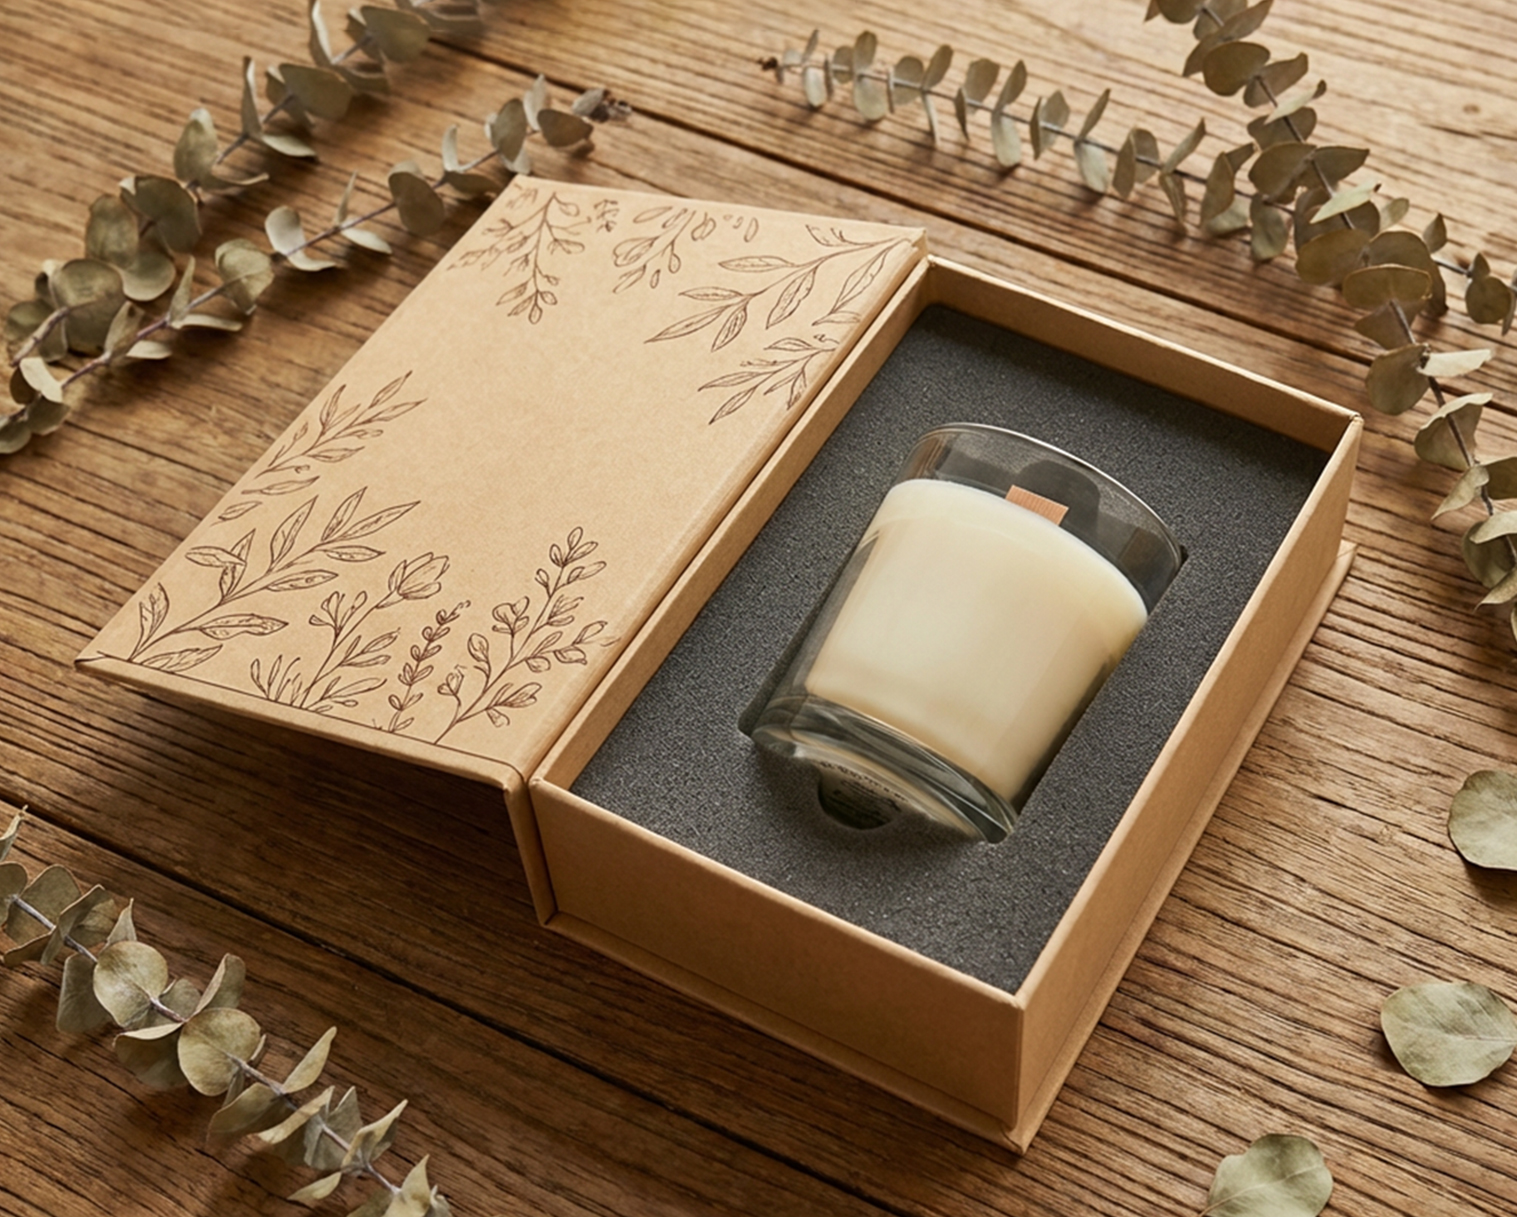
Folding Carton Material and Board Selection
Selecting the correct cartonboard grade and mechanical specifications prevents line failures, controls material cost, and maintains structural integrity across the supply chain.
Comparison of Primary Cartonboard Grades
Different applications demand distinct structural performance. Choosing the wrong grade compromises shelf impact and causes downstream converting failures. The four primary commercial grades:
- Solid Bleached Sulfate (SBS): Pure bleached chemical pulp, white throughout. Offers the highest surface smoothness, print fidelity, and embossing performance. Standard for cosmetics, spirits, and pharmaceutical cartons.
- Folding Boxboard (FBB): Multi-ply board with mechanical pulp sandwiched between chemical pulp layers. Delivers high stiffness-to-weight ratio, reducing material cost while maintaining rigid panel structures.
- White-Lined Chipboard (WLC): Manufactured from recovered recycled fibers with a clay-coated white top layer. Economical for dry goods packaging where direct food contact is not required.
- Solid Unbleached Sulfate (SUS): Unbleached virgin kraft fibers providing high tear resistance and compression strength. Used for heavy beverage carriers and industrial transit packaging.
Accurate board specification requires evaluating five physical attributes:
- Basis Weight (gsm): Board mass per square meter, directly impacting package weight and material cost.
- Caliper (microns / points): Board thickness. Panel stiffness scales cubicly with caliper, so small increases yield major rigidity gains.
- Stiffness (Taber units): Resistance to panel bowing under high-speed filling equipment loads.
- Surface Smoothness: Determines ink transfer quality and foil-stamping registration accuracy.
- Grain Direction: Board is stiffer parallel to the grain. Align grain with load-bearing panels for structural stability.
Application Engineering and Converting Compatibility
The product environment and converting machinery dictate board specifications. A substrate designed for dry storage will underperform in chilled or humid conditions.
- Direct Food Contact: Requires certified virgin SBS or FBB with water-based dispersion barriers or polymer lamination to prevent grease migration and package softening.
- Frozen and Chilled Products: Coated boards with moisture-resistant barriers prevent fiber weakening during condensation and thawing cycles.
- Pharmaceuticals: Dimensionally stable, high-whiteness boards ensure legible barcode printing, accurate serialized code scanning, and clean braille embossing.
- Cosmetics and Premium Goods: Smooth SBS board withstands hot foil stamping, deep debossing, and spot UV without surface failure.
Converting compatibility requires upfront coordination. インクの塗布量が多い, UV varnishes, and film laminations can prevent adhesive bonding on glue flaps. Designers must map glue keep-out zones on the dieline and keep adhesive areas free of all coatings to ensure strong seams on the folder-gluer. Creasing also demands attention: fold cracking — where the outer coating ruptures and exposes raw fibers — typically occurs when thick board folds against the grain or when low humidity makes the coating brittle. Match crease rule height and matrix width to exact board caliper, and validate with physical prototypes before production.
On the sustainability front, high-bulk FBB allows caliper and basis weight reduction without sacrificing panel stiffness. Specify certified fibers from FSC, PEFC, or SFI channels, and limit hard-to-separate polymer laminations and oversized plastic windows so the carton breaks down cleanly in standard paper recycling streams. For a deeper look at how packaging regulations affect material choices, see our article on PPWR-compliant packaging requirements.
Printing and Finishing Options for Folding Cartons
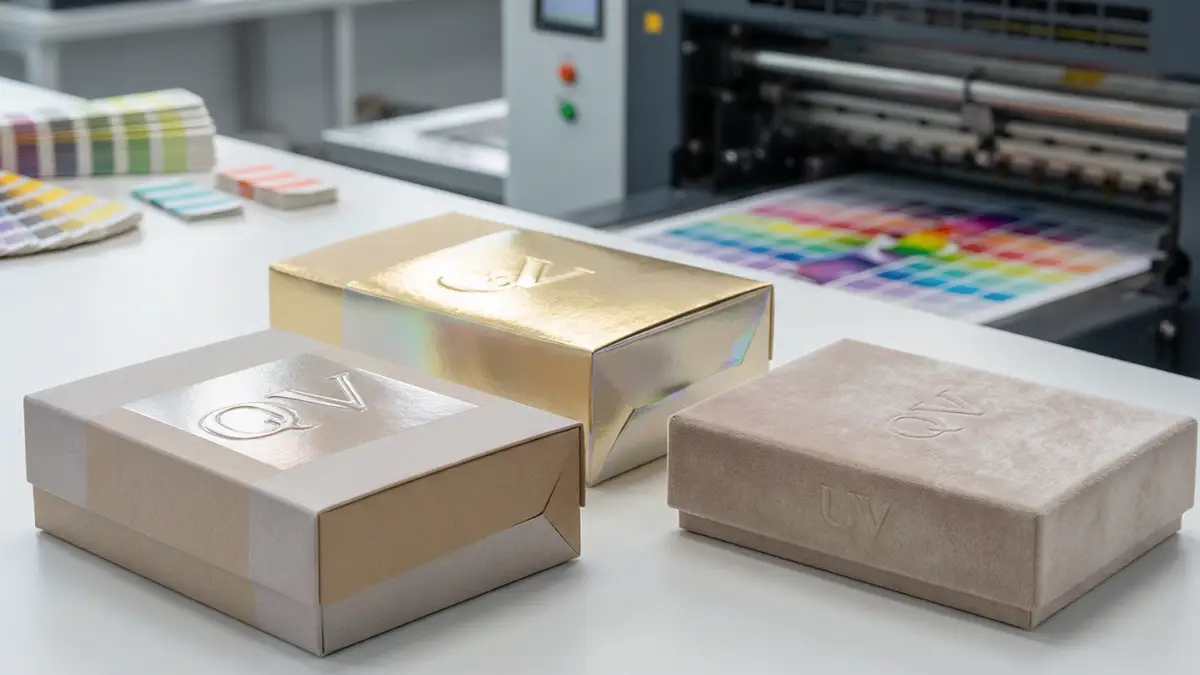
Matching print methods and finishing chemistry to run volume and substrate prevents cracking, ensures regulatory compliance, and controls unit cost.
Primary Printing Methods and Ink Technologies
Select printing processes based on run volume, substrate surface, and graphic complexity. The right combination ensures ink adhesion and balanced production cost.
- Offset Lithography: Best for medium to high volumes on coated boards such as SBS. Delivers high image resolution and precise color registration; requires plate setup.
- フレキソ印刷: Suited for very high volumes on unbleached kraft or recycled substrates. Runs fast and adapts to uneven surfaces, though fine detail loses sharpness versus offset.
- デジタル印刷: Ideal for short runs, prototypes, and versioned packaging with variable data. Eliminates plate setup costs entirely.
Ink chemistry determines shelf appearance and safety compliance beyond standard CMYK process:
- Spot Colors: Standardized Pantone inks deliver exact brand color consistency across runs and eliminate shifts in large solid-color panels.
- Metallic Inks: Metal-particle formulations provide reflective accents at lower cost than foil, though without mirror-like brightness.
- Low-Migration Inks: Engineered for food-contact and pharmaceutical cartons to prevent ink chemicals from migrating through the board to the product.
For direct food contact, low-migration inks are reinforced with physical barrier layers — extruded polyethylene, dispersion coatings, or internal liners — to stop grease and moisture migration.
Finishing Techniques and Structural Conversion
Finishing treatments protect printed graphics from scuffing during transit and create visual contrast on the retail shelf.
- Aqueous Coatings: Water-based, applied inline during printing. Dry quickly, protect against rub damage, available in gloss or matte.
- UV Coatings: Cured under ultraviolet light for high-gloss protection. Spot UV applied selectively highlights logos against matte backgrounds.
- ソフトタッチ仕上げ: Velvety tactile effect, popular for cosmetics and premium personal care packaging.
Decorative finishes that add physical relief or metallic reflection require specialized tooling:
- フォイルスタンピング: Heat, プレッシャー, and metal dies transfer metallic film. Keep foil details away from glue zones to prevent adhesive failure.
- エンボス加工 / デボス: Raises or sinks graphics by altering the board profile. Relief depth must match board thickness and fiber direction to avoid tearing.
The final conversion phase — die-cutting, scoring, and gluing — depends on three parameters: major crease lines must run parallel to grain (folding against grain causes coating split); score depth and width must match exact board caliper (shallow scores cause crooked folds, deep creases rupture outer fibers); and glue flaps must remain free of all inks, varnishes, and foils for strong fiber-tearing bonds on the folder-gluer.
Industry-Specific Folding Carton Design Needs
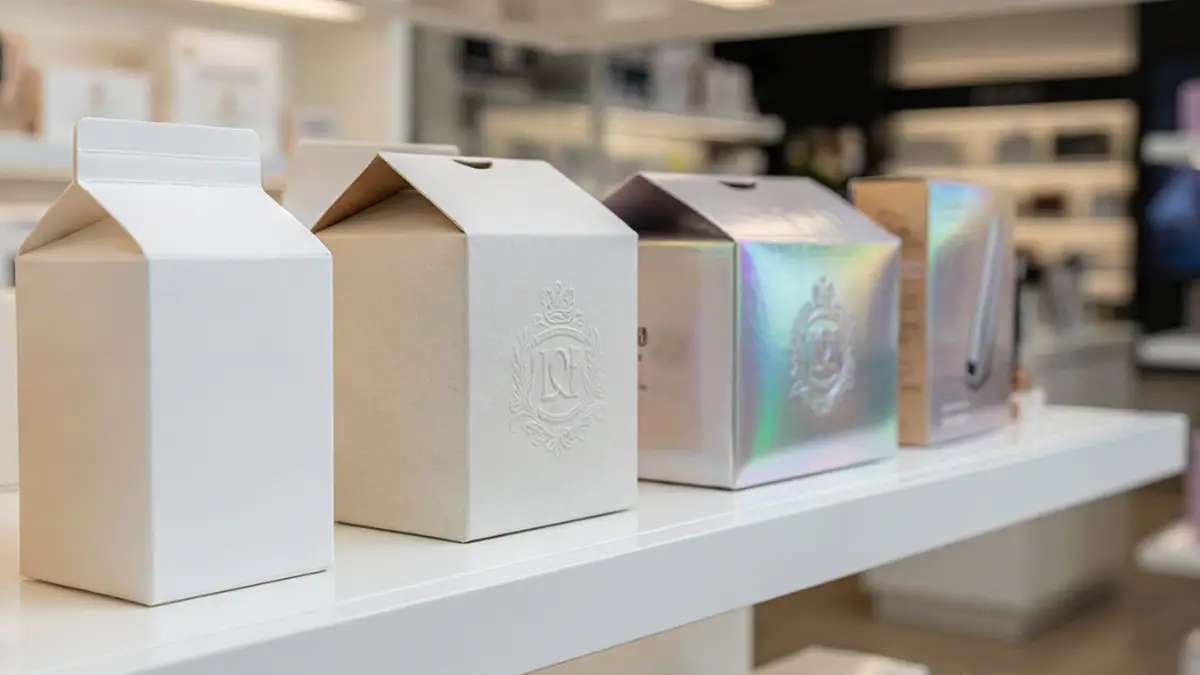
Every product category introduces unique physical demands and regulatory requirements. A carton designed for retail shelves will underperform in parcel networks or cleanrooms unless you design for those parameters from the start.
Sector-Specific Functional and Regulatory Constraints
- 食品包装: Food-contact-compliant boards, barrier treatments (ワックス, polyethylene, dispersion coatings), and grease-resistant coatings to prevent moisture and oil migration.
- Pharmaceutical Cartons: Strict text legibility, serialization quiet zones, dimensional consistency for automated filling, and optional tamper-evident seals or braille.
- Cosmetic and Premium Packaging: High-quality SBS or FBB supporting detailed color reproduction, 箔押し, エンボス加工, and gloss coatings.
- Consumer Electronics: Protective interior structures — paperboard inserts, folded partitions, auto-bottom bases — to prevent component damage.
- E-commerce Packaging: Reinforced corners, secure locking closures, and higher compression strength for drop impacts and mechanical sorting during parcel distribution.
Material Specifications and Performance Testing
Structural decisions must rest on physical testing data, not unverified digital templates.
- Board Selection: Match product mass to caliper, stiffness, and grammage — typically 270 – 350 GSM for premium and food cartons using SBS or FBB.
- Prepress Preparation: 3 mm bleed on outer cut edges, designated glue exclusion zones, and careful graphic positioning to avoid fold-line cracking.
- 表面仕上げ: Water-based coatings, UV varnishes, and laminations provide moisture resistance but must be tested to confirm they do not impair gluing or recyclability.
- Verification Protocols: Test compression strength, パフォーマンスを落とす, vibration resistance, and ink scuffing using production-grade board, 接着剤, and coatings — not generic prototypes.
Running physical trials with production materials exposes score cracking and glue failures before tooling commitment. Understanding the broader landscape of box materials and manufacturing capabilities also helps — our overview of corrugated box manufacturers in China covers how different structural formats serve different product categories.
How to Choose a Folding Carton Manufacturer
Evaluating a packaging supplier requires auditing technical tolerances, material supply chains, and total landed costs — not just comparing unit-price quotes.
Technical Capabilities and Quality Standards
Your design must translate from digital file to physical assembly without warping, line slowdowns, or aesthetic failure. Technical vetting covers four areas:
| Vet Area | What to Verify | なぜそれが重要なのか |
|---|---|---|
| デザイン & Prototyping | CAD dieline creation, 3D simulation, unprinted white sample workflow | Catches structural conflicts before production tooling is cut. |
| 印刷する & 仕上げる | Sheet-fed offset + デジタル, G7 color management, in-house die-cutting and folding-gluing | Single-source accountability from artwork to finished carton. |
| 認証 | ISO 9001 (品質システム), BRCGS (food-contact), FSC / PEFC (fiber sourcing) | Required for regulated industries and brand compliance programs. |
| Material Traceability | Lot-level board tracking, humidity-controlled storage, dual-sourced mills | Prevents batch variation and supply disruption. |
Operational Capacity and Commercial Terms
Unit price tells only part of the story. Production volume, procurement structures, and supply resilience determine your final packaging ROI.
- Lead Times & Scalability: Track prepress, tooling, and converting schedules across seasonal peaks to identify capacity bottlenecks.
- Total Landed Cost: Compare MOQs, setup charges, delivery, and storage costs rather than analyzing unit price alone.
- Facility Audits: Verify humidity control in board storage, raw material lot-traceability, and housekeeping standards on-site.
- Supply Resilience: Confirm dual-sourced board mills, backup press options, and written change-control policies.
Typical Procurement Workflow
A structured ordering process prevents specification drift between sample approval and bulk delivery:
| ステージ | What to Lock Down | なぜそれが重要なのか |
|---|---|---|
| 1. 構造サンプル | Unprinted white sample in target caliper — test dimensions, fold clearance, 製品のフィット感. | Validates geometry before any print investment. |
| 2. Printed Proof | Color-accurate proof on production board — verify artwork, Pantone matches, and finish effects. | Locks brand color and regulatory copy before bulk run. |
| 3. Production Trial | Small batch on production tooling — confirm folder-gluer runnability and glue bond strength. | Catches tooling issues before full commitment. |
| 4. Bulk QC | Pre-shipment inspection against frozen specs — AQL sampling for dimensions, print, and closure performance. | Ensures batch consistency with approved samples. |
よくある質問
What file format should I submit for folding carton dieline design?
Submit a press-ready PDF (PDF/X-1a or PDF/X-4) alongside the editable Adobe Illustrator (.ai) file. Keep the manufacturer-issued structural dieline on its own locked layer, with all vector cut, crease, and fold lines using spot colors set to overprint at 100% 規模.
How do I calculate the correct board weight for my product?
Select a target grammage (通常 200 – 400 gsm) based on product weight and shelf requirements. Multiply grammage by the flat blank area in square meters. 例えば, ある 0.1092 m² blank at 300 gsm weighs approximately 32.8 grams before coatings or adhesives.
What is the difference between offset and digital printing for folding cartons?
Offset printing uses physical plates, making it economical for medium-to-long runs with precise Pantone spot colors and maximum consistency. Digital printing outputs directly from electronic files, offering faster turnaround and lower cost for short runs, multiple SKU variations, and serialized graphics.
What is the typical minimum order quantity for custom folding cartons?
MOQ typically ranges from 100 に 500 単位. Digital printing supports short runs of 50 – 300 単位, while offset printing and complex finishing operations (window patching, エンボス加工) generally require 300 – 1,000 units to amortize setup costs.
How long does it take from dieline approval to mass production delivery?
Domestic production typically requires 2 – 6 weeks from final proof approval to delivery. Repeat orders using existing dies can arrive in 1 – 4 週. International orders should allow 10 – 16 weeks to accommodate production, customs clearance, and ocean transit.
最終的な考え
Skipping technical validation on a folding carton design saves nothing in practice. A single jammed folder-gluer or split score line on your filling erases any upfront savings within hours of production downtime. Specifying the correct SBS or FBB caliper, validating fold allowances with physical mockups, and auditing your manufacturer’s converting capabilities are the three steps that reliably prevent these failures.
Start with an unprinted structural sample in your target caliper to test fold geometry and line clearance before committing to tooling. 私たちのチームに連絡してください to request a sample kit or submit your dieline files for a technical review.